Detonation Gun (D-Gun) Thermal Spray Coating at Shafel Tech
PIONEERING HIGH-PRECISION SURFACE COATING SINCE 2000 • ISO 9001:2015

Advanced Thermal Spray & Detonation Gun Coatings

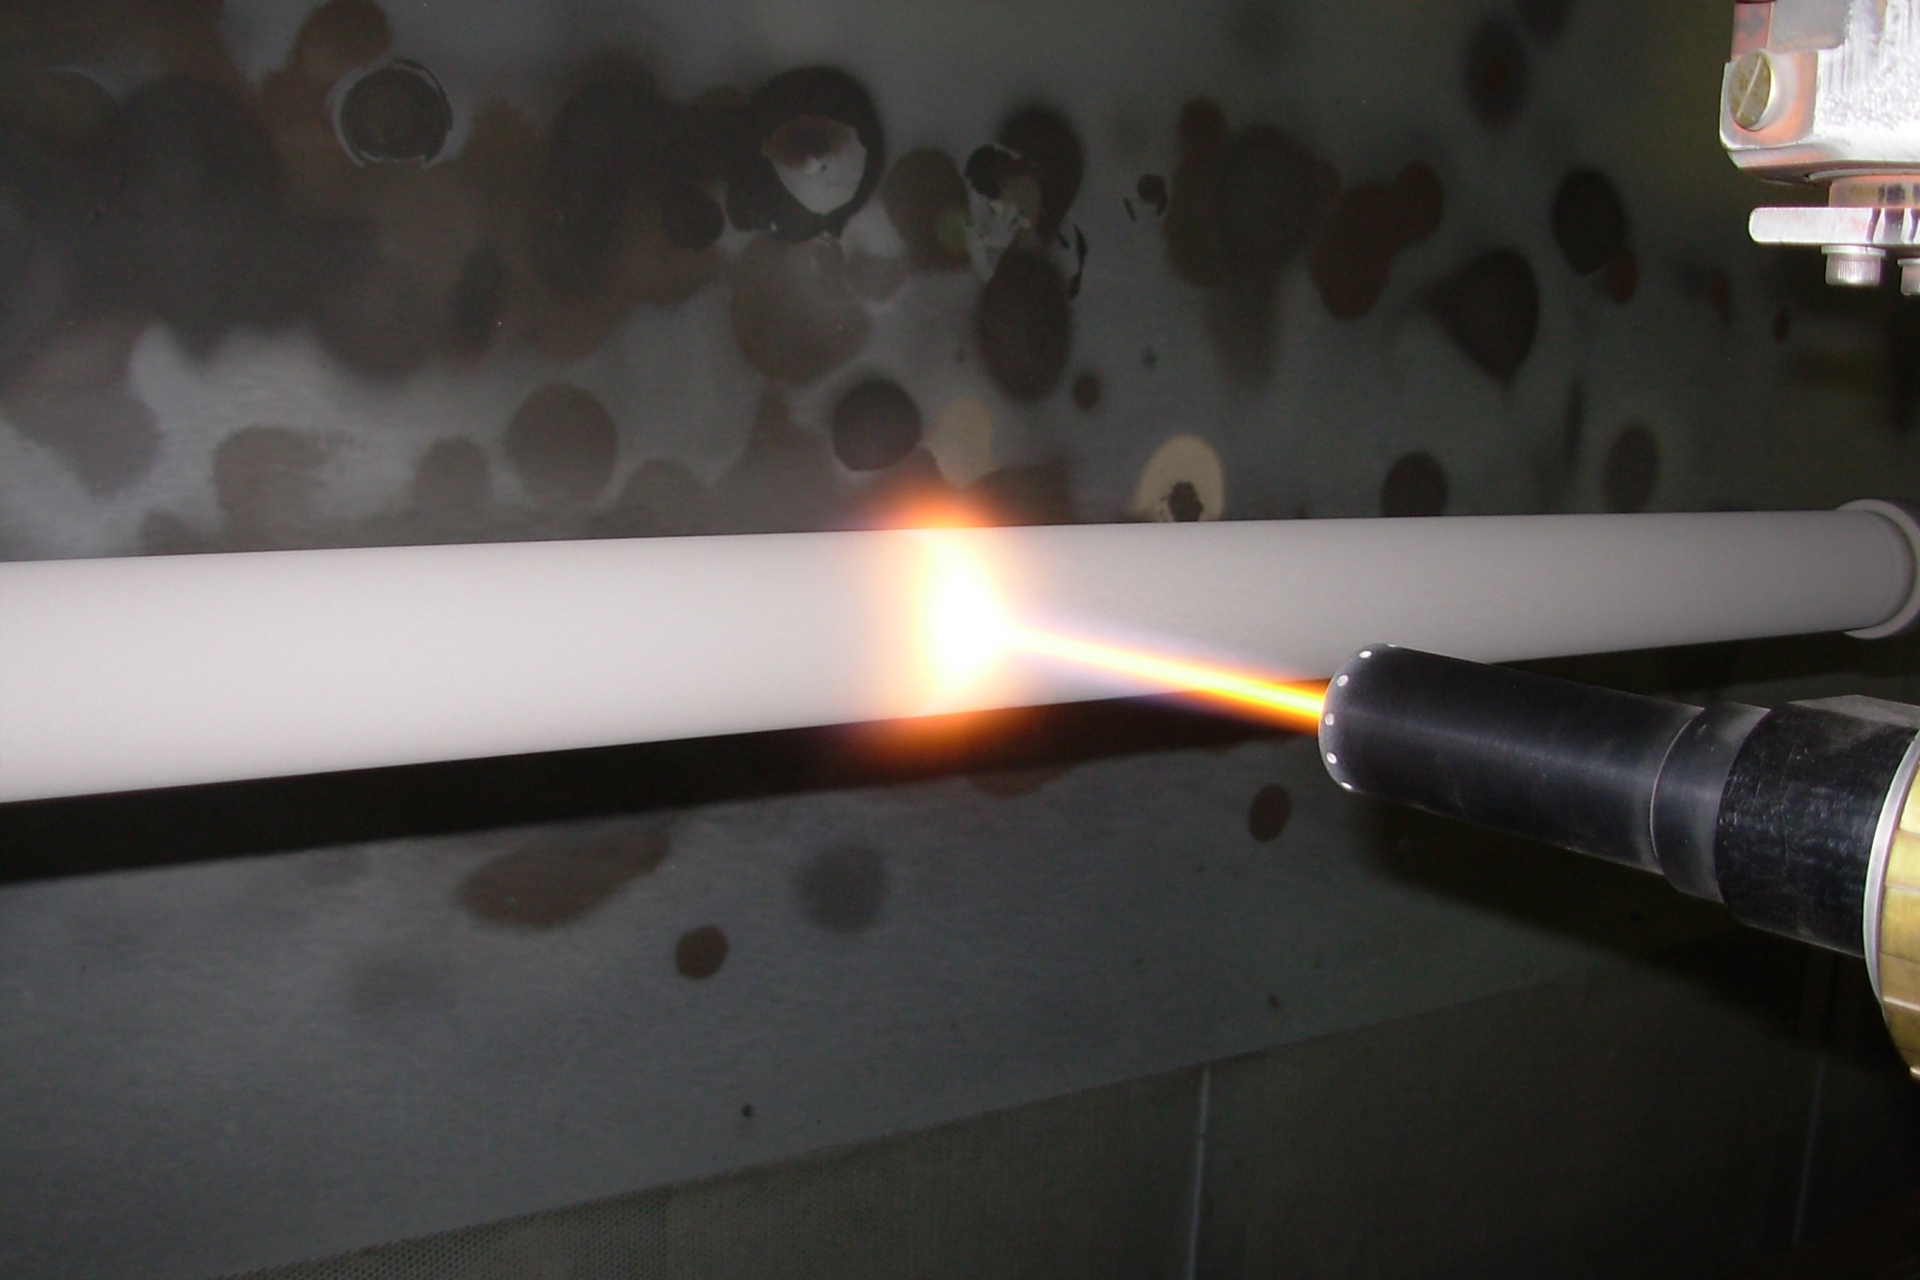
Robotic High Velocity Oxy-Fuel (HVOF) Process
SUPERSONIC KINETIC IMPACT • 7-ROBOTIC MANIPULATION

Robotic High Velocity Oxy-Fuel (HVOF) Systems

Thermal Spray Zinc and Molybdenum Coating
CATHODIC CORROSION DEFENSE • LOW-FRICTION TRIBOLOGY

Thermal Spray Zinc, Aluminum

Turbine Component Reconditioning and Precision Grinding
TURNKEY SALVAGE • DEFENSE & AEROSPACE ACCREDITED

Component Reconditioning & Precision Grinding

20+
Years Of Excellence
10,000+
PSI Bond Strength
1,250HV
Hashable-by-Maximum
HAL Approved
Aerospace Supplier Since 2000
Trusted Partnerships

Trusted By Premier Aerospace, Energy & Industrial Leaders Across India

Client Partner 1
Client Partner 2
Client Partner 3
Client Partner 4
Client Partner 5
Client Partner 6
Client Partner 7
Client Partner 8
Client Partner 9
Client Partner 10
Client Partner 11
Client Partner 12
Client Partner 13
Client Partner 14
Client Partner 15
Client Partner 16
Client Partner 17
Client Partner 18
Client Partner 19
Client Partner 20
Client Partner 21
Client Partner 22
Client Partner 23
Client Partner 24
Client Partner 25
Client Partner 26
Client Partner 27
Client Partner 28
Client Partner 29
Client Partner 30
Client Partner 31
Client Partner 32
Client Partner 33
Client Partner 34
Client Partner 35
Client Partner 36
Client Partner 37
Client Partner 38
Client Partner 39
Client Partner 40
Client Partner 41
Shafel Tech Manufacturing and Coating Facility

24+

Years Of Industrial Mastery

ISO 9001:2015 Quality Benchmarking

Welcome to Shafel Tech

Established in 2000, Shafel Tech caters to high-stress manufacturing sectors for mission-critical thermal spray coating requirements. We deploy the world’s most advanced surface modification technologies, notably Detonation Spray Coating (D-Gun) and Robotic HVOF Systems.

D-Gun coatings deliver the highest adhesion bond strength in the industry with the absolute lowest substrate temperature heating. This prevents metallurgical phase distortion and ensures micro-dimensional accuracy on delicate turbine airfoils, thin-walled pump sleeves, and precision shafts.

Zero Component Distortion & Thin Substrate Integrity

Lowest substrate thermal input prevents warpage or micro-structural degradation of critical tolerances.

Bond Strength Surpassing 10,000 PSI

Supersonic gas detonation locks carbide and ceramic particles deep into the metal matrix.

Comprehensive In-House Reconditioning

Welding arc welding, Stellite cladding, and precision cylindrical roller grinding up to 2.5m length.
Our Strategic Vision

To pioneer world-class surface engineering solutions that extend industrial component operational lifespan by 400% to 1000%, eliminating premature downtime.

Our Engineering Mission

To provide high-integrity, cost-effective reconditioning and wear barrier solutions with uncompromising turnaround schedules and strict ISO standards.

Our Quality Commitment

Continuous investment in robotic automation, precision CNC manipulation, and metallographic test equipment to ensure flaw-free Coating and repeatability.

SURFACE MODIFICATION ENGINEERING

Our Core Coating Technologies

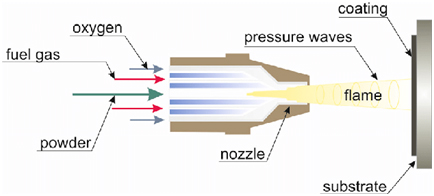
Detonation Gun (D-Gun) Coating Schematic
Flagship Proprietary

Detonation Gun (D-Gun) Coating

Combines combustible fuel gas and powder inside a water-cooled detonation chamber. Supersonic shockwaves propel particles at hypersonic velocities for extreme mechanical interlocking into the substrate.

  • Zero distortion on thin airfoils & impellers
  • Supersonic detonation shockwave (3,000 m/s)
  • Highest bond density among thermal spray methods
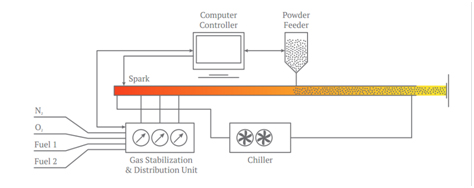
Robotic HVOF System Schematic
Robotic Automation

High Velocity Oxy-Fuel (HVOF) System

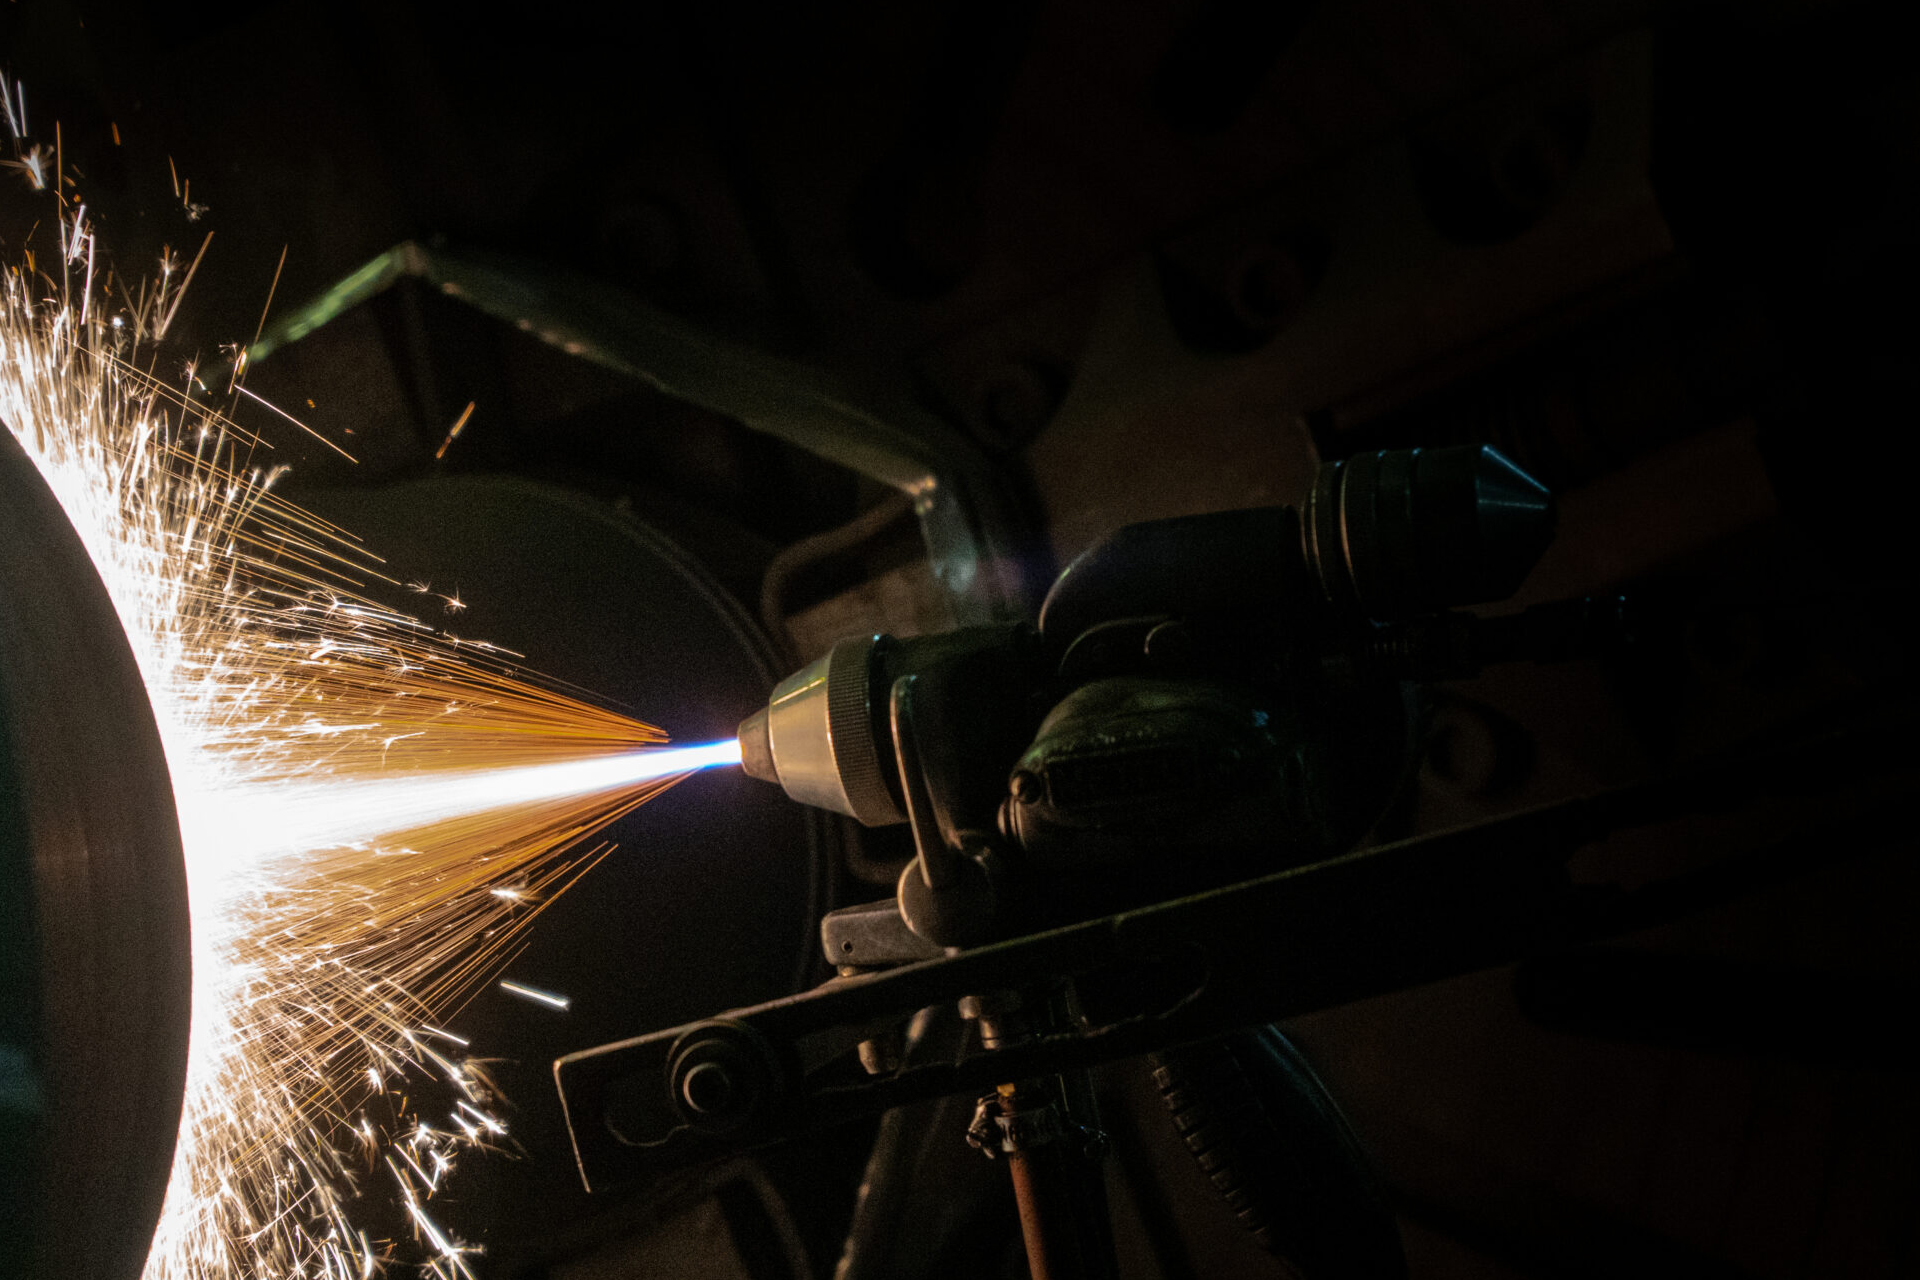
High-pressure oxygen and fuel gas continuous combustion through a Laval nozzle produces supersonic jet velocities of Mach 2 to 3. Ejected powders impact the substrate with immense kinetic energy.

  • Superior electrolytic hard chrome alternative
  • High compressive residual stress for fatigue life
  • Near-theoretical density (99.5% solid)
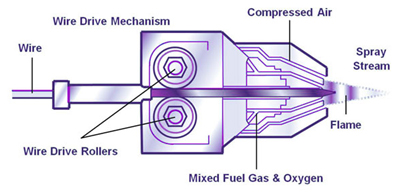
Wire Flame Spray Process
Galvanic & Thermal Barrier

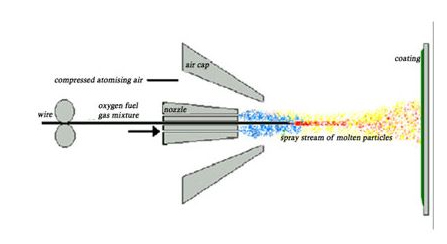
Wire Flame Spray Process

Continuous wire feedstock (Aluminum, Zinc, Bronzes) is fed through a concentric nozzle, melted by oxygen-fuel flame, and atomized by compressed air. Ideal for large structural components.

  • Long-life atmospheric corrosion protection
  • Zinc & Aluminum sacrificial passivation
  • Babbitt metal bearing sleeve relining
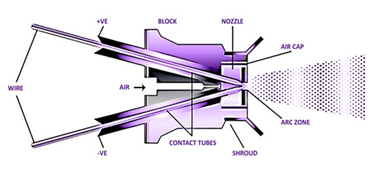
Twin Wire Arc Spray Process
Cold Deposition Metallizing

Twin Wire Arc Spray Process

Two conductive wires are brought together under electrical potential, igniting an electric arc that melts both tips simultaneously. Air atomization propels fine droplets with minimal base metal heat.

  • Thick deposits for deep mechanical rebuilds
  • Negligible substrate heating eliminates warping
  • High spray rate for large industrial rolls
Plasma Transferred Arc (PTA) Process
True Metallurgical Fusion

Plasma Transferred Arc (PTA)

PTA overlay welding utilizes superhard cobalt-based Stellites and nickel cermets melted directly into the parent metal via a constricted plasma column, ensuring 100% metallurgical bonding.

  • Severe erosion and high-temp valve seating
  • Zero risk of spalling under brutal point impact
  • Stellite 6, Colmonoy & Tungsten Cermets
Nitriding and Boronizing Diffusion
Thermochemical Diffusion

Nitriding & Boronizing Treatment

Thermochemical diffusion process saturating the steel matrix with interstitial nitrogen and boron. Elevates surface hardness past 1400 HV while maintaining tough, ductile core properties.

  • Complete galling prevention on hydraulic shafts
  • Zero dimensional distortion during treatment
  • Dramatic friction reduction on sliding journals
Comprehensive Engineering Spectrum

Our Precision Engineering Services

Thermal Spray Processes

Full-suite specialized coatings utilizing D-Gun, robotic HVOF, wire arc, and flame spray to defeat abrasion, chemical attack, and extreme thermal conditions.

  • Detonation Gun (D-Gun) Coatings
  • Robotic HVOF Tungsten Carbide
  • Metal Flame Spraying & Arc Metallizing
  • High-Temperature Corrosion Barriers

Reconditioning & Rebuilding

Reclaiming worn shafts, rollers, and valves to original blueprint dimensions at a fraction of the cost and lead time of procuring new assemblies.

  • Submerged Metal Arc Welding
  • Stellite & Superalloy Cladding
  • Precision TIG, MIG & Arc Welding
  • Shaft Journal Rebuilding

Manufacturing & Machining

Heavy-duty in-house machine shop handling cylindrical grinding up to 2.5 meters length and heavy lathes up to 3.2 meters length.

  • Cylindrical Roller Grinding (700mm x 2.5m)
  • Precision Lathes (700mm x 3.2m)
  • Mirror Superfinishing ( 0.1 Ra)
  • Dynamic Balancing & Quality Inspection
Plant Infrastructure

Product Handling & Heavy Machining Capacity

3.0 M
Max Component Length Capacity
1.5 M
Max Job Diameter Capacity
Multiple Access
HVOF Robot (25kg Payload, 2m Reach)
2.5 M
Cylindrical Roller Grinding Length

Have Heavy or Complex Geometries?

Our facility can accommodate large-scale industrial rolls up to 1.5m diameter and shafts up to 3.2m length.

Schedule a Plant Inspection
Direct Technical Inquiry

Connect With Our Metallurgical Experts

Visit our Thirumudivakkam manufacturing works or reach our dedicated Production Coordinators directly.

Manufacturing Facility Address

No: 1, SIDCO Industrial Estate, Thirumudivakkam,
Chennai - 600 132, Tamil Nadu, India.

Direct Phone Lines

Production Co-Ordinator: +91 93840 50341
Admin / Purchase Dept: +91 95512 99512

Operational Working Hours

Monday - Saturday: 8:30 AM – 7:30 PM IST
Emergency Technical Callout: 24/7 Available

FROM OUR COMPANY PRESENTATION

Explore Our Coating Projects, Components & Facilities

Browse the full image gallery, coating processes, industry applications and manufacturing facilities from the Shafel Tech presentation.

View Complete Portfolio